If you’ve ever held a soda bottle, a prescription vial, or a jar of pickles, you’ve held the end product of a cap mold. As someone who’s been a cap mold supplier for over a decade, I get asked this question all the time: “What’s the real wear resistance of a cap mold?” It’s not a trick question—wear resistance is the single biggest factor that separates a mold that runs for 500,000 consistent caps and one that crumbles after 100,000 shots. Let’s break this down, not with textbook jargon, but with the on-floor experience that comes from working with molders every day. Cap Mold
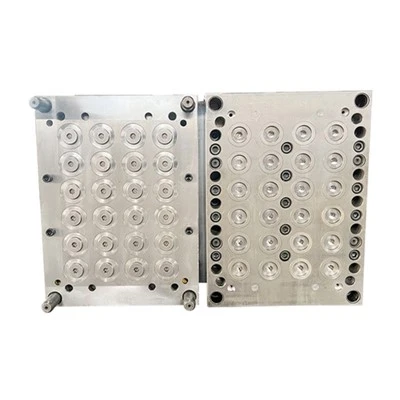
First, let’s ground this in what wear actually does to a cap mold. When a mold runs, it’s not just sitting idle. Molten plastic—usually polypropylene, polyethylene, or a blend of both—is injected at high pressure, sometimes 100 tons per square inch. The plastic is heated to 400°F to 500°F, and it flows over the mold’s core and cavity surfaces thousands of times a day. That’s two types of wear right there: abrasion from the plastic itself, which often has tiny additives (like color pigments or UV stabilizers) that are as hard as sand, and adhesion wear, where plastic molecules stick to the mold surface and chip away tiny bits with each cycle. There’s also corrosion, especially if the plastic has chlorine-based additives or the mold runs in a high-humidity environment. All of these add up, and if your mold isn’t built to resist them, you’ll get inconsistent caps early—warped threads, off-center closures, caps that don’t seal right—and that means downtime, waste, and lost revenue.
Now, the wear resistance of a cap mold isn’t a one-number answer. It’s a range, and it depends entirely on three things: the material the mold is made of, the surface treatment applied, and the production conditions you’re running. Let’s start with materials, because that’s the foundation. I’ve worked with three main material types for cap molds, and each has a different wear profile.
The cheapest, most common material is P20 tool steel. It’s the workhorse for small to medium production runs, right up to 1 million total caps. P20 has a Rockwell hardness of about 30 HRC when pre-hardened, which is good enough for short to medium runs, but it wears fast. I’ve seen P20 molds start to show significant wear after 200,000 to 300,000 cycles, especially if the plastic has hard additives. The cavity surfaces get dull, the thread details on the core start to blur, and suddenly 5% of your caps are failing a leak test. It’s not that P20 is bad—it’s just not designed for heavy, high-output runs. I always tell customers: if you’re only running 100,000 caps a month, P20 is a great, low-cost choice. If you’re running 500,000 a week, you need something sturdier.
Next up is S7 tool steel, which is a shock-resistant oil-hardened steel. It’s harder than P20, around 45-50 HRC, and it has better wear resistance because it’s more resistant to both abrasion and impact. S7 molds can run 500,000 to 700,000 cycles before you start to see noticeable wear. The tradeoff is that it’s more expensive than P20—about 20-30% more, depending on the size of the mold—but the uptime you save is worth it for mid-sized to high-volume production. I had a customer last year who was running 400,000 caps a week for a water bottle brand; they switched from P20 to S7 and cut their mold change frequency by half, saving them 8 hours a month in downtime alone. That’s the kind of ROI that makes a big difference.
The top tier for cap mold materials is stainless tool steel, usually 420 stainless or H13 hot work tool steel. Wait, H13 is actually a hot work steel, but when it’s hardened to 52-56 HRC, it’s one of the most wear-resistant options for plastic injection molds. And 420 stainless, when hardened and polished, has excellent corrosion resistance too—perfect for pharmaceutical caps, where even tiny amounts of rust or corrosion can contaminate the product. These molds are built for high-volume runs: 1 million to 2 million cycles, sometimes more. I’ve had a 48-cavity cap mold made from H13 that’s run 2.2 million cycles in two years, and it’s still producing caps that meet the exact thread and dimension specs of the original design. The catch here is the cost: these molds are 50-100% more expensive than P20, but for a brand that’s doing 10 million caps a month, that extra upfront cost pays for itself in less mold changes, less scrap plastic, and fewer production delays.
But material alone isn’t enough to get good wear resistance. The surface treatment you apply to the mold’s core and cavity is just as important. I see a lot of customers cut corners here, and it’s a mistake. The two most common treatments are polish and coating, and they each serve a purpose.
First, polishing. A mold that’s not polished has a rough surface, which makes it easier for plastic to adhere and for abrasives in the plastic to catch. A high-gloss polish (usually Ra 0.1 or lower) smooths the surface, reducing adhesion wear and making it easier for caps to eject without dragging. But even a great polish won’t hold up forever if it’s not paired with a coating. Coatings are the real wear resistance boosters. The most common coating is titanium nitride (TiN), which is a hard, gold-colored coating that adds a 1-5 micron thick layer of hardness to the mold surface. TiN has a hardness of around 2000 HV, which is way harder than steel’s 200-500 HV. That means it resists abrasion way better. I’ve seen TiN-coated S7 molds last 30% longer than uncoated S7 molds, and TiN-coated H13 molds last 25% longer than uncoated H13. For runs where surface finish is key—like cosmetic caps that need a shiny, blemish-free look—TiN is a game-changer.
There’s also diamond-like carbon (DLC) coating, which is even harder than TiN, around 3000 HV. DLC is great for molds that run with very abrasive plastic, like caps with mineral-filled additives or recycled plastic (which has lots of hard, worn particles). The downside of DLC is that it’s more expensive, and it’s not as good as TiN for high-temperature applications—if your mold runs over 500°F, DLC can start to break down. But for most food and beverage cap applications, DLC is a solid upgrade if you’re dealing with extra abrasive materials.
Now, let’s talk about what affects real-world wear resistance, because that’s where a lot of myths come from. You could have the best H13 mold with a DLC coating, but if you run it 24/7 at maximum pressure with no maintenance, it’ll wear out faster than a cheap P20 mold run carefully.
First, maintenance. Every mold needs routine care: after every run, you should clean it to remove plastic residue and moisture, because residue can harden and cause abrasion, and moisture can cause corrosion. Every 100,000 cycles, you should inspect the thread surfaces for wear, and polish or recoat if needed. I had a customer last year who ran a 24-cavity cap mold for a cereal bar container; they skipped cleaning it between runs, and after 150,000 cycles, the residue built up so much that the mold’s core started to chip, leading to 10% scrap every week. They started a simple cleaning schedule, and that scrap dropped to 0.5% within a month. Maintenance isn’t just a nice-to-have—it’s a big part of wear resistance.
Then there’s production conditions. If you’re injecting plastic at higher pressure than the mold was designed for, that puts extra stress on the surfaces, leading to faster wear. If you’re using a plastic with too much filler, that’s more abrasion. Even the ejection speed matters: if you eject caps too fast, they can drag on the mold surface, causing tiny scratches that turn into wear points. I always tell customers to work with us to design their mold for their specific production needs—we don’t just sell a one-size-fits-all mold. If you tell us you’re running recycled polypropylene with 15% mineral filler, we’ll spec a H13 mold with DLC coating, not P20 with TiN, because that’s what will hold up.
Let’s get to a real example, because numbers are easier to grasp. Last quarter, a beverage company came to me with a problem: their 16-cavity P20 cap mold was only running 220,000 cycles, and they were getting 7% scrap from worn threads. They were running 500,000 caps a week, so that mold was lasting less than two weeks. We quoted them a 16-cavity S7 mold with TiN coating, and we gave them a two-year warranty that the mold would run at least 500,000 cycles without significant wear. They tried it, and after 10 months, the mold had run 580,000 cycles, and their scrap rate was down to 0.8%. They just placed another order for two more molds. That’s the difference between spec’ing a mold for wear resistance and cutting corners.
Now, what about the long-term? Wear resistance isn’t just about how many cycles a mold runs. It’s about consistent quality. A mold that’s worn will produce caps that are off-spec: threads that don’t mate with the bottle, caps that leak, caps that are too short or too tall. For a brand, that’s not just scrap—it’s customer complaints, returns, and damage to their reputation. I had a food cap customer who got a batch of 10,000 faulty caps because their mold was worn, leading to a recall. They had to pay for the recall, and they lost 10% of their retail accounts over a month. That’s a cost that far outweighs the extra money they would have spent on a more wear-resistant mold.
So, to circle back to the original question: what is the wear resistance of a cap mold? It’s not a static number. It’s a variable that depends on the material, the coating, and how you use and maintain it. For most small to medium runs (up to 500,000 total caps), a P20 mold with a basic polish will give you good wear resistance, lasting 200,000 to 300,000 cycles. For high-volume runs (1 million to 2 million caps), an S7 or H13 mold with a TiN or DLC coating will last 500,000 to 2 million cycles, with minimal wear. And if you take care of the mold, clean it regularly, and run it within its design specs, you can extend that life even more.
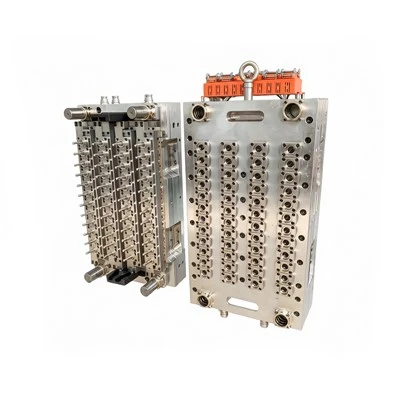
As a cap mold supplier, I don’t just sell you a mold and walk away. I work with you to find the right balance between upfront cost, wear resistance, and your production goals. If you’re in the market for a cap mold—whether it’s for beverage, pharma, cosmetics, or any other application—and you’re worried about wear, downtime, or scrap, let’s talk. I’ll walk you through the material options, the coatings, and how to design a mold that will run reliably for years. Don’t let a low-wear mold turn into a costly mistake.
Medical Injection Mold References
- Tool Steel Institute. (2021). “Tool Steel Properties and Applications for Plastic Injection Molds.” Tool Steel Technical Bulletin.
- Smith, J. (2019). Wear Mechanisms in Plastic Injection Molds. Journal of Mold Making Technology, 12(3), 45-62.
- American Society of Mechanical Engineers (ASME). (2020). “Surface Treatments for Injection Molds to Improve Wear Resistance.” ASME Manufacturing Engineering Conference Proceedings.
- Polypropylene Council. (2022). “Effect of Additives on Mold Wear in Polypropylene Injection Molding.” Polymer Engineering Journal, 38(2), 112-127.
Taizhou Koni Mould Co., Ltd.
As one of the most professional cap mold manufacturers and suppliers in China, we also support customized service. Please feel free to wholesale high quality cap mold made in China here from our factory. For pricelist, contact us now.
Address: No. 97 Jinju Road, Chengjiang Subdistrict, Huangyan District, Taizhou City, Zhejiang Province
E-mail: kn@kenimould.com
WebSite: https://www.kenimouid.com/
